
Can you automate where the air can ignite?
Yes, but not with standard equipment.
With flammable vapours or combustible dust in the air, a motor, a panel or a hot surface is an ignition source. What applies is equipment built for that atmosphere.
What it is
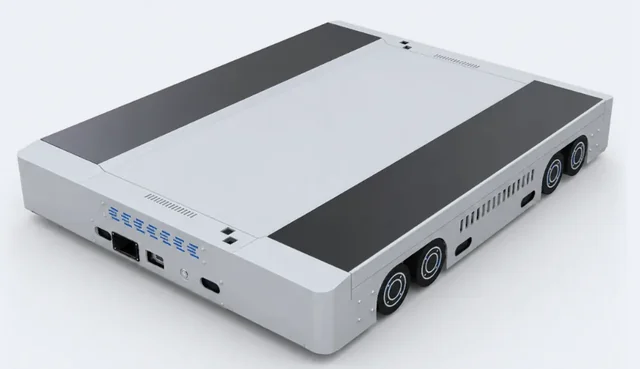
ATEX is short for explosive atmospheres, the category of equipment made to work where the air can ignite. The cart does the same as the standard shuttle, but it is built not to produce sparks, electric arcs, hot surfaces or static electricity.
Keep reading
It is not an add-on: the motor, enclosure, wiring and materials all change.
In practice
A warehouse with solvent vapour or airborne dust can be automated with the version of the shuttle robot prepared for explosive atmospheres. The project always starts from the zone classification signed by your plant’s health and safety specialist.
Keep reading
Without that classification there is no project.
What an ATEX shuttle robot is, and what the abbreviation means
Where the risk appears: warehouses that are a classified zone without anyone saying so
The best known cases are liquids: warehouses holding solvents, paints, alcohols, aerosols and agrochemicals, where the vapour given off by the product mixes with the air and forms an atmosphere that can ignite. A badly closed container, a decanting operation or a spill is enough for the concentration to rise in one particular area.
Keep reading
The second group takes people by surprise, because it has no smell: combustible dust. Flour, sugar, starch, milk powder, aluminium, wood, coal. Once that dust is suspended in sufficient concentration it behaves like a gaseous fuel, and a single spark is enough. Worse still, the dust settled on structures and light fittings is thrown up by a first small explosion and feeds a second, larger one. That is why in dry food or metal powder warehouses the question is not whether protected equipment is needed, but in which areas and how severely.
What changes inside the machine: a list of things that must not happen
It helps to read the ATEX version backwards: not as a list of special components, but as a list of things the cart is forbidden to produce. There must be no electrical spark, so motors and control panels are built differently and the wiring stops being ordinary wiring.
Keep reading
There must be no hot surface, so the machine is designed to dissipate the heat it generates and the temperature any exposed part can reach is limited. There must be no mechanical spark, so materials and contact pairs are chosen that do not spark when they rub or knock together. There must be no build-up of static electricity, so wheels, guides and structure are earthed in a way nobody looks at on an ordinary shuttle. And battery charging, a particularly sensitive moment, is resolved outside the classified area. Exact conditions and certifications for the chosen equipment come with the diagnosis.
Without a zone classification there is no project
The drawing comes before the machine. The zone classification is the document stating which part of the warehouse may hold an explosive atmosphere, with which substance, how often and for how long.
Keep reading
It is signed by a health and safety specialist on the client side, someone who knows the products, the decanting operations, the ventilation and the history of the plant. STOKA starts from that document: we neither replace it nor estimate it. It is the only way for the equipment going into the warehouse to match the real risk rather than an assumption. If the classification has not been done yet, that is the first step of the project, and a step to be taken anyway, with automation or without it, because it also governs the electrical installation, the lighting and the floor equipment. With the zone drawing in hand, the survey becomes a technical conversation instead of a list of assumptions.
What does not change: the storage logic is the same
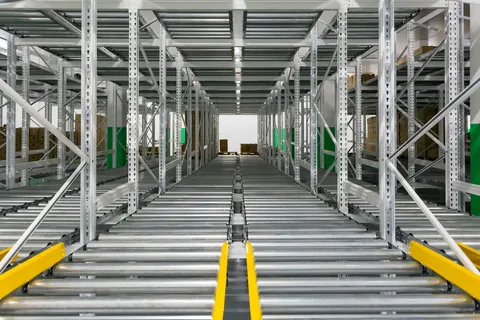
It is worth spelling out, because it raises doubts: the explosive-atmosphere version is not a different system. The storage logic is the same as the shuttle robot, the cart still enters the channel, the density gained is the same — within the ranges STOKA works with, up to three times the current one, with up to 66% of the floor freed up — and so is the software, with the same traceability and the same record of every movement.
Keep reading
Automated systems still work between 7 and 40 metres of height and installation still takes 3 to 4 months from the purchase order. What changes is how the equipment is built and the engineering work done beforehand. With hazardous goods, traceability also carries a value of its own: knowing exactly what is held, how much and where is part of managing the risk, not only the stock.
What defines a shuttle project in an explosive atmosphere?
We do not publish model-by-model specification tables: the detailed sheet comes with the assessment, sized against your operation. These are the criteria the choice is made on.
The zone classification, first of all
It is the input the project starts from and your health and safety specialist provides it. It settles which areas need protected equipment and how severely. Without that document nothing is sized: it is estimated, which is exactly what must not happen.
Gas and vapour, or combustible dust
Not the same problem. Solvent vapour disperses and concentrates near its source; dust settles, is thrown up again and can feed a second explosion. Protecting the equipment is resolved differently in each case.
How much of the warehouse is really classified
It is rarely all of it. If the area at risk is a limited one, the sensible move is to automate the rest with standard equipment and treat that area separately. Over-equipping a whole warehouse raises the cost without adding safety.
Maintenance, spare parts and battery charging
Protected equipment is serviced differently: some tasks are not done inside the area and battery charging is resolved outside it. Look at this during layout, because it settles routes and service areas.
Volume per reference still rules
The atmosphere settles what the equipment has to be like, not whether it suits you. If volume per reference does not fill the channel, a shuttle is not justified, ATEX or otherwise. The underlying criterion does not change.
When is an ATEX shuttle robot the wrong answer?
When the risk can be removed instead of lived with.
Improving ventilation, changing the packaging or moving the flammable product to a separate area often costs a fraction of certified equipment and truly lowers the risk. If the classified zone is small, it is better to automate the rest with standard equipment. And the limits of any shuttle apply: many SKUs with low volume are not its ground.
Frequently asked questions
Can't find your question?Write to us and we reply within one business day.
Tell us about your case01What does ATEX mean?
It is short for explosive atmospheres (ATEX). It covers equipment built to work where the air may hold gases, vapours or flammable dust in a concentration high enough to ignite. ATEX equipment is not reinforced equipment: it is equipment designed so that it cannot produce a spark, an electrical arc or a hot surface.
02Does STOKA classify the zones of my warehouse?
No. The classification is signed by a health and safety specialist on your side, someone who knows the products, the decanting operations and the ventilation of the plant. We take it as an input and size the system on that basis. Without a classification there is no project, and that is not a formality.
03Do I lose density or functions compared with an ordinary shuttle?
No. Storage logic, density and software are the same: up to three times the current density, up to 66% of the floor freed up and the same inventory record. What changes is how the equipment is built and the engineering needed beforehand to specify it properly.
04What if only one area of my warehouse is a classified zone?
That is the most common case and usually good news. The rest is automated with standard equipment and that area is handled separately, either with protected equipment or on manual operation with its own procedures. The boundary between zones is settled in the layout, alongside the classification.
Bring the zone drawing andwe will talk about equipment
The survey starts from your zone classification and settles which area needs protected equipment, which is automated with standard equipment and what is better left manual. With that we deliver layout, technical sheet and quotation.