
Why does the warehouse fill up with aisles?
Because every conventional rack needs an aisle, and the aisle stores nothing.
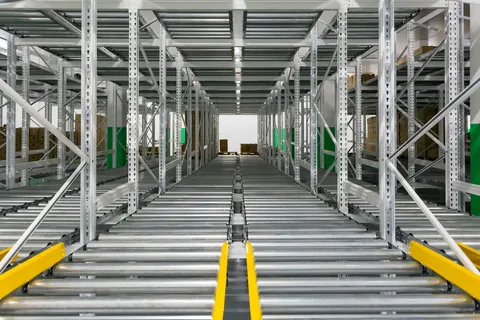
When a cart moves inside the channel, one lane serves many positions in depth, and that floor goes back to storing stock.
What it is
It is a motorised cart that runs inside the racking instead of along the aisle. It takes the load at the mouth of the channel, carries it to the back and sets it down; to retrieve it, it does the reverse.
Keep reading
Within the ranges we work with, it can triple density and free up to 66% of the occupied floor.
In practice
The shuttle robot moves inside the rack channel, so one access lane is enough for many positions in depth. There are versions for pallets and for totes, variants for cold storage down to −25 °C and versions for explosive atmospheres.
Keep reading
It pays when the volume per SKU fills the channels.
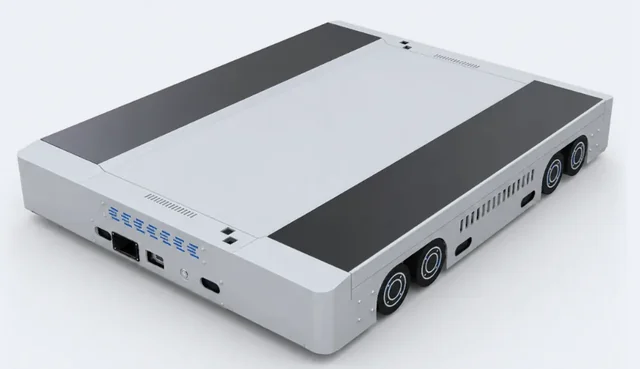
What a shuttle robot, also called a satellite cart, actually is
Movement variants: what each cart can actually do
Not every cart does the same job, and the difference shows up in the layout. The simplest ones travel back and forth in a single direction: they enter the channel, drop off or collect the load and return to the mouth.
Keep reading
Moving them to another channel takes an operator with a forklift, or a piece of equipment that repositions them. Four-way carts travel both along the channel and across it, so they change aisle under their own power and, with a lift, change level as well: the system stops being a set of separate channels and starts behaving like a grid. The third variant is the mother-and-child arrangement: a large cart, the mother, runs along a main lane and carries a smaller cart, the child, to the mouth of the channel, and the child is the one that goes in for the load. Which one suits you depends on how many channels you have to serve per hour and on how much transfer time is worth in your operation.
Cold: how far the shuttle goes, and where it stops
A shuttle robot works down to −25 °C, and that figure is a design limit rather than a preference. Below it, everything changes: the battery delivers less, lubricants thicken, the electronics turn sensitive, and the condensation of moving in and out of the chamber starts doing damage.
Keep reading
If your cold store runs colder than −25 °C the shuttle is not the answer, and it is worth saying so before quoting: the pallet stacker crane, the machine that travels along the aisle and lifts the load to its position, goes down to −30 °C. That is why the figure to bring to the survey is not the nominal temperature of the chamber but the real working one, measured at the coldest point and at the worst moment of the cycle. It also matters whether the load crosses from cold to ambient zones, because that crossing determines protection, defrost cycles and maintenance frequency. Exact conditions for the chosen equipment are set out in the technical sheet of the diagnosis.
ATEX: warehouses where the air itself can catch fire
Some warehouses hold an atmosphere that can ignite. It happens where the air carries vapours from solvents, alcohols, paints or aerosols, or fine dust in suspension: flour, sugar, wood, aluminium.
Keep reading
In those conditions a spark or a hot surface is enough to start an explosion, and ordinary electrical equipment cannot be inside. That is what ATEX versions are for, an abbreviation that refers to explosive atmospheres: carts with protected enclosures on motors and control panels, surface temperature control, materials that do not spark on friction, earthing and static control, and battery charging outside the classified zone. Classifying the zone, which area is at risk, with which substance and how often, is an input the client provides through their own risk assessment; we do not estimate it. Nor is the whole warehouse usually a classified zone, so protected equipment in the critical sector plus standard equipment everywhere else is often enough. Little material on this circulates in Spanish, so we analyse it during the survey with your safety officer and put it in writing in the diagnosis.
Beyond the mouth of the channel: how the system is integrated
The cart is half the system. The other half is what happens at the mouth of the channel and in the software.
Keep reading
Something has to bring the load there: a forklift, a conveying line, or a stacker crane that also moves the cart between levels, and that choice changes overall performance as much as the cart itself does. On the digital side you need software that knows which position of which channel holds each pallet and in what order they should come out, integrated with your warehouse management system (WMS). On the building side come the floor, the electrical supply, the battery charging area and the protection of the structure. Automated storage systems work between 7 and 40 metres of height, and installation takes 3 to 4 months from the purchase order. We do not publish model-by-model tables: the full technical sheet is delivered with the diagnosis, already calculated for your own warehouse.
What is a pallet shuttle, and how does a 4-way shuttle differ?
A pallet shuttle, or shuttle robot, is a motorised cart that runs inside the racking channel: it takes the pallet at the mouth, carries it to the back and sets it down, so the forklift never drives into the rack.
A 2-way shuttle only travels along its channel; a forklift or transfer car moves it to the next one. A 4-way shuttle also travels crosswise along service aisles and changes channel by itself, and with level-changing lifts one robot can reach any position in the block. The 2-way version is simpler and suits few SKUs with many pallets each; the 4-way version automates the whole block, with more complex structure and software.
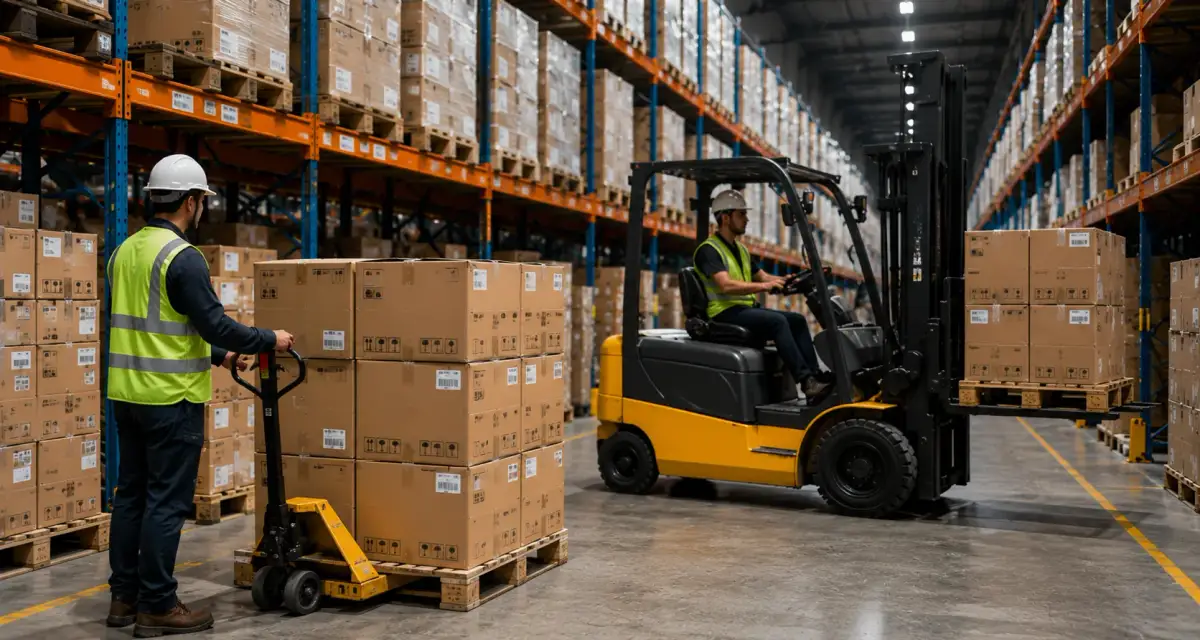
Pallet shuttle advantages and disadvantages
What it gains: density, by removing the aisles between rows; less forklift travel; and operation in cold rooms down to −25 °C.
Within the ranges we work with, it can triple density. What it costs: each channel holds a single SKU, so many low-volume SKUs waste half-filled channels; access is no longer direct, and the retrieval order depends on whether a channel is loaded and unloaded from the same face or from opposite faces; and the system relies on batteries and software that are sized together with the structure.
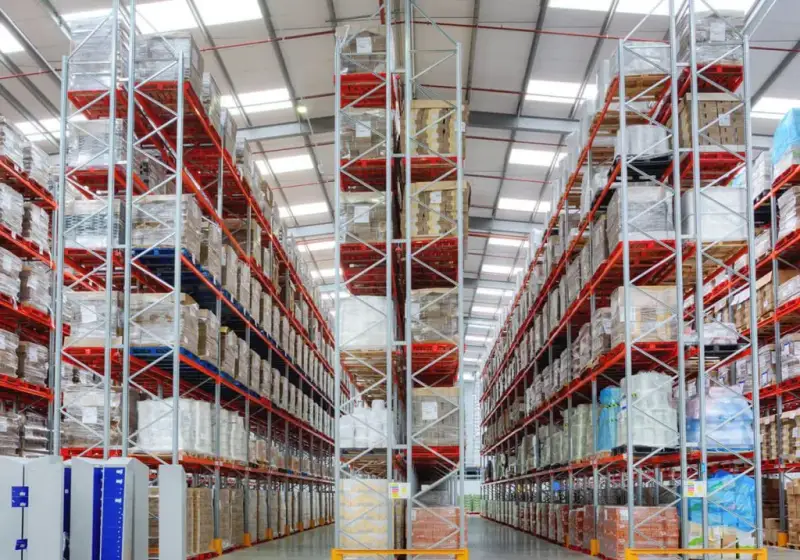
What decides whether a shuttle robot is the right answer?
We do not publish model-by-model specification tables: the detailed sheet comes with the assessment, sized against your operation. These are the criteria the choice is made on.
Volume per reference
A channel is filled with a single reference. If the volume of each one is not enough to fill a whole channel, the density you gain on paper is lost in half-empty channels that take up the whole space anyway.
Load unit: pallet or case
Moving full pallets is not the same as moving cases and plastic containers for piece picking. They are two different scales of system, each with its own structure, software and working rhythm, and it is worth settling before looking at any equipment.
Required despatch sequence
A channel with access from one side only gives back the last thing that went in. If you work with expiry dates or batches and need the oldest goods out first, plan for channels with access at both ends, or combine them with selective positions.
Working temperature and atmosphere
The shuttle goes down to −25 °C and the pallet stacker crane to −30 °C. If there are also vapours or flammable dust in the air, the conversation moves to versions for explosive atmospheres (ATEX) and to zone classification.
Real clear height and floor condition
Automated systems work between 7 and 40 metres. Height is measured to the lowest interfering point, not to the roof. Floor flatness and permissible load are verified on site, because they decide whether the cart runs evenly.
When is a shuttle robot the wrong answer?
It does not pay if you need to reach any pallet right away.
Density is paid for in access: the channel order must be respected, and if your operation needs everything now, that order becomes waiting. Nor with low volume per SKU, because a half-full channel takes the whole channel. And if the cold room runs colder than −25 °C, other equipment applies.
Frequently asked questions
Can't find your question?Write to us and we reply within one business day.
Tell us about your case01How does a shuttle robot differ from a stacker crane?
The stacker crane travels along the aisle and lifts the load to its position; the shuttle cart travels inside the channel, horizontally. One gives direct access to every position at height, the other gives density in depth. Cold changes too: the pallet stacker crane goes down to −30 °C and the shuttle to −25 °C.
02What is a pallet shuttle?
It is a shuttle robot: a motorised cart that works inside the racking channel, carrying pallets from the mouth to the back and out again. It gains density because the forklift no longer enters the channel. It is also called a satellite cart or radio shuttle.
03What is a 4-way shuttle?
It is a shuttle that, besides running along the channel, travels crosswise on service aisles and changes channel on its own. With lifts between levels it can serve any position in the block, which automates the entire store rather than a single channel.
04Does it work in a frozen storage chamber?
It depends on the real working temperature. Down to −25 °C, yes. If the chamber runs colder than that, other equipment applies: the pallet stacker crane goes down to −30 °C. Measuring the coldest point, at the worst moment of the cycle, is part of the survey and settles the system before any other consideration.
05Are there versions for warehouses with solvents or flammable dust?
Yes. There are carts built for explosive atmospheres (ATEX), with protection on motors and control panels, surface temperature control and battery charging outside the classified zone. Zone classification comes from your own risk assessment; we take it as an input and size the system on that basis.
06How long does installation take, and what do I get before deciding?
Installation of automated systems takes 3 to 4 months from the purchase order. Before that you receive the survey, the layout and the technical sheet of the proposed system, calculated for your warehouse. We do not publish capacity or speed tables out of context, because they lead people to buy the wrong thing.
Other systems
Before quoting a shuttle,the channel has to be measured
The survey settles channel depth, load unit, real working temperature and floor condition. With that we deliver the layout, the technical sheet and the quotation. And if racking is enough for you, we say so.